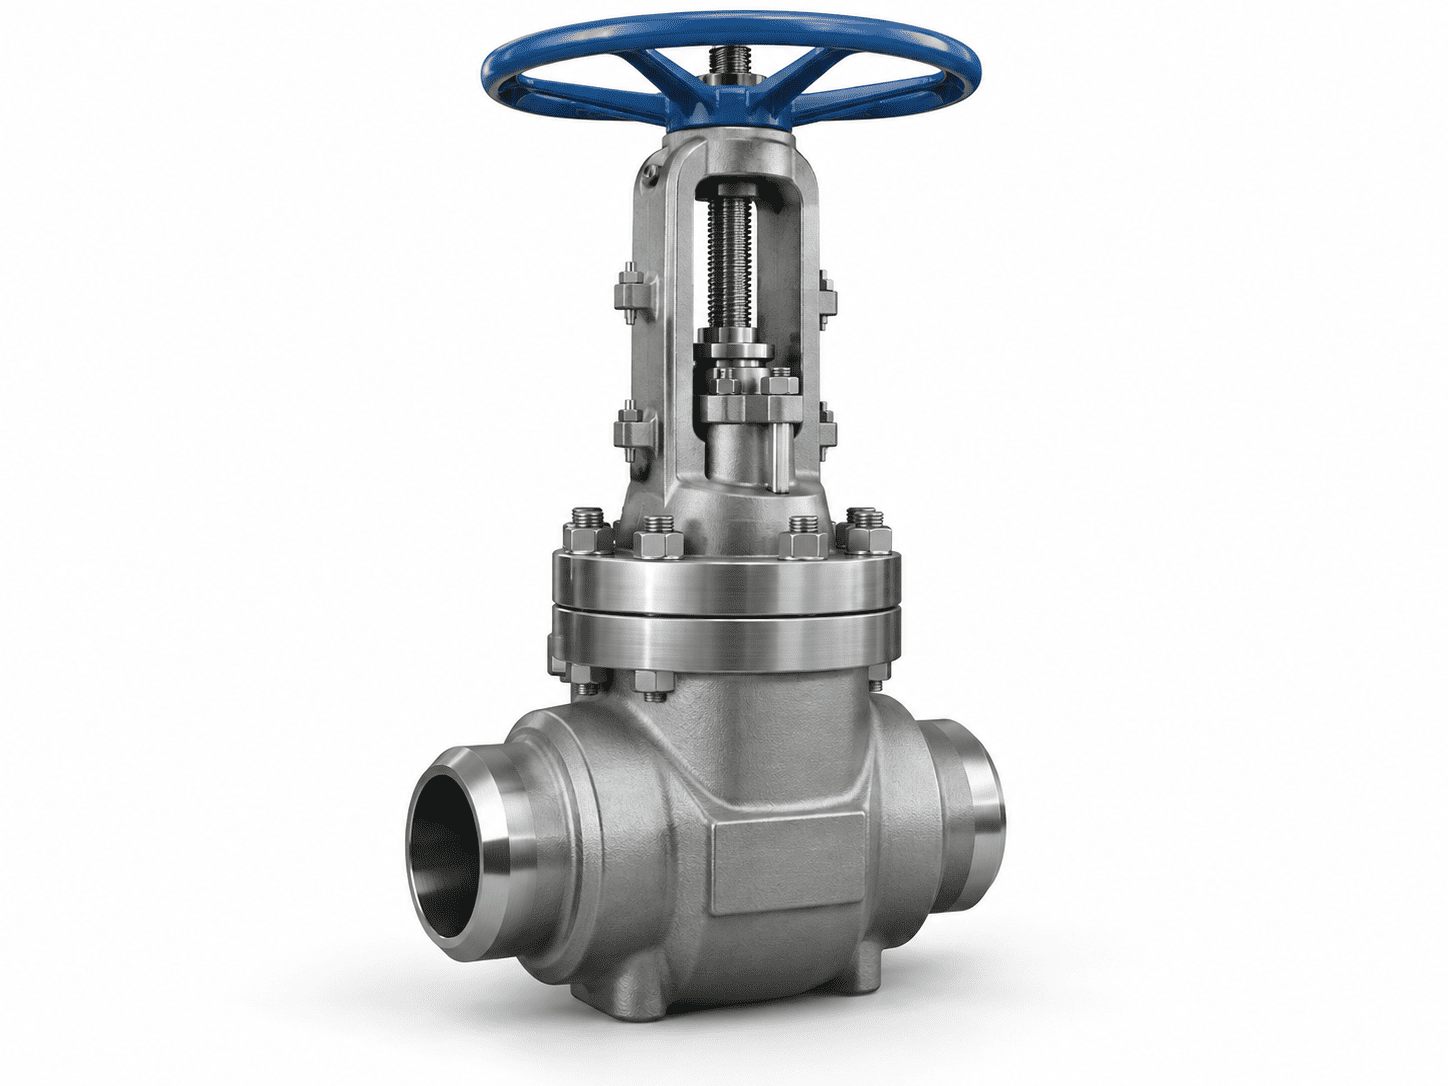
DN100 Class 2500 Gate Valve: A Power Plant RFQ Case
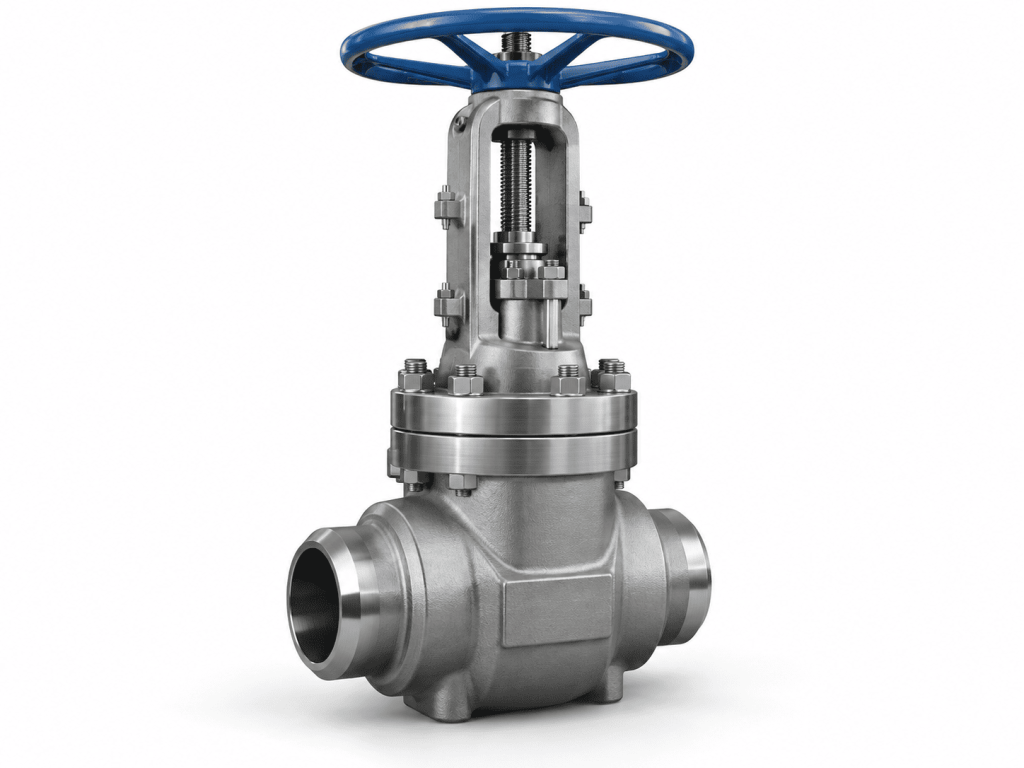
The inquiry calls for one double disc / parallel slide gate valve for a high-pressure power plant requirement. Its value as a purchasing case lies in the combination of a defined closure design, alloy body and trim materials, welded piping interfaces and twenty technical and documentation requirements. A quotation needs to reconcile all of these points rather than simply match size and pressure class.
This page presents the requested specification and the engineering information needed to develop an offer. Operating medium, pressure, temperature, final operator selection and acceptance records have not been supplied. It is therefore an RFQ-based application case; it does not report a completed delivery or demonstrated plant performance.
For the wider product family, see the Vcore industrial gate valve range. The existing Pressure Seal Gate Valve page explains the general bonnet construction; this case focuses on the specific Class 2500 procurement schedule.
What Makes This Configuration Different?
Parallel Slide Closure
The RFQ specifies double discs and parallel seating geometry. A conventional wedge gate is a different configuration and requires buyer approval if proposed as an alternative.
C12A Pressure Body
ASTM A217 C12A identifies a cast material requirement. A forged F91 body must be identified as a proposed substitution, with a revised material schedule.
F91 Hardfaced Trim
Disc and seat substrates are specified as F91 with Stellite overlays. The offer should identify both the base materials and the precise hardfacing specification.
PSB Configuration Review
The buyer requests a pressure seal bonnet if available. The quotation must resolve this option into an explicit offered construction.
Weld-End Compatibility
DN100 alone does not define the final welding interface. Pipe outside diameter, wall thickness and approved end preparation are needed.
Traceable Acceptance
Material, dimensional and test records should be tied to the supplied valve identity and agreed inspection plan.
Technical Specifications from the Inquiry
| Specification Item | Requested Configuration / Confirmation |
|---|---|
| Valve type | Double disc / parallel slide gate valve |
| Application | Power plant high-pressure isolation; exact line and medium to be confirmed |
| Size and quantity | NPS 4 / DN100; 1 piece |
| Pressure designation | ASME Class 2500; service-specific pressure-temperature rating required |
| Body | ASTM A217 Grade C12A, cast construction |
| Discs | ASTM A182 Grade F91 with Stellite hardfacing |
| Seats | ASTM A182 Grade F91 with Stellite hardfacing; attachment design to be confirmed |
| Stem | ASTM A479 Type 410; suitability to be reviewed against actual duty |
| Bonnet | Pressure seal bonnet requested if applicable / available; final configuration to be confirmed |
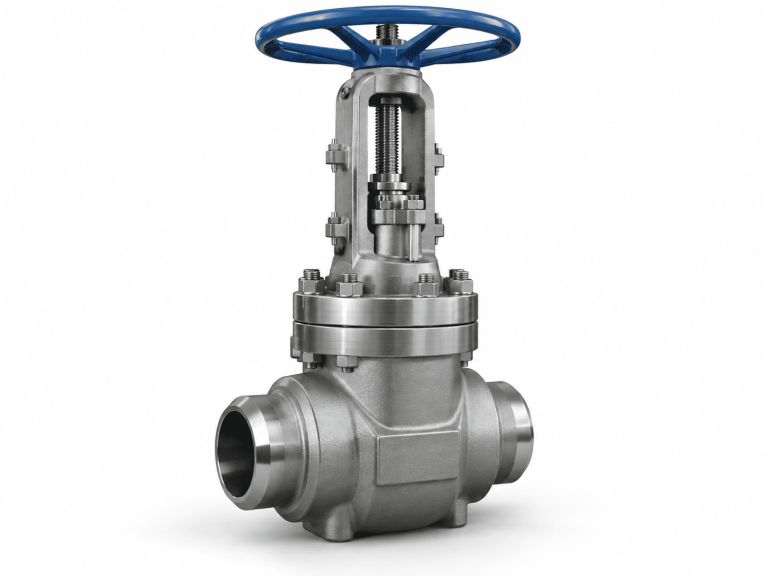
| Ends | Butt weld, with end preparation according to ASME B16.25 |
| Design basis | ASME B16.34; API 600 or equivalent requested, with scope and PSB applicability clarified |
| Operating conditions | Medium, normal/design pressure and temperature, startup conditions and maximum differential pressure required |
| Operation | Not specified; operator type, loads and access requirements to be confirmed |
| Dimensions and weight | Approved GA drawing, end-to-end length, bore, installed height, maintenance clearance and actual weight required |
| Testing and documents | Inspection procedures, MTC, pressure and seat test records, COO and COC; additional examinations as agreed |
How the Parallel Slide Design Is Reviewed
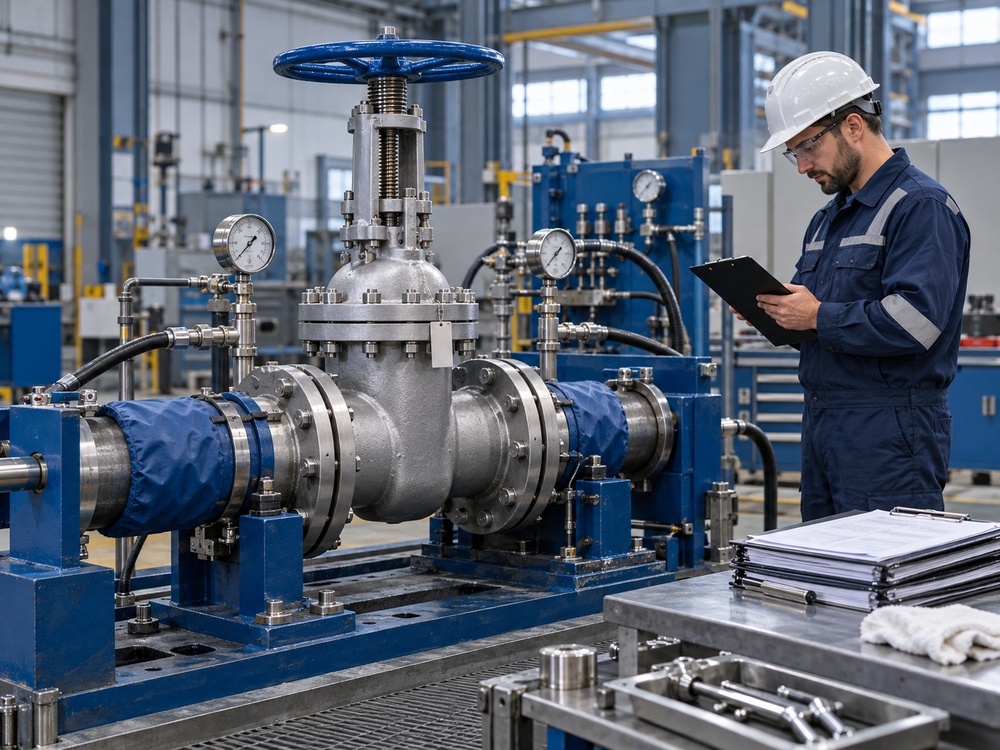
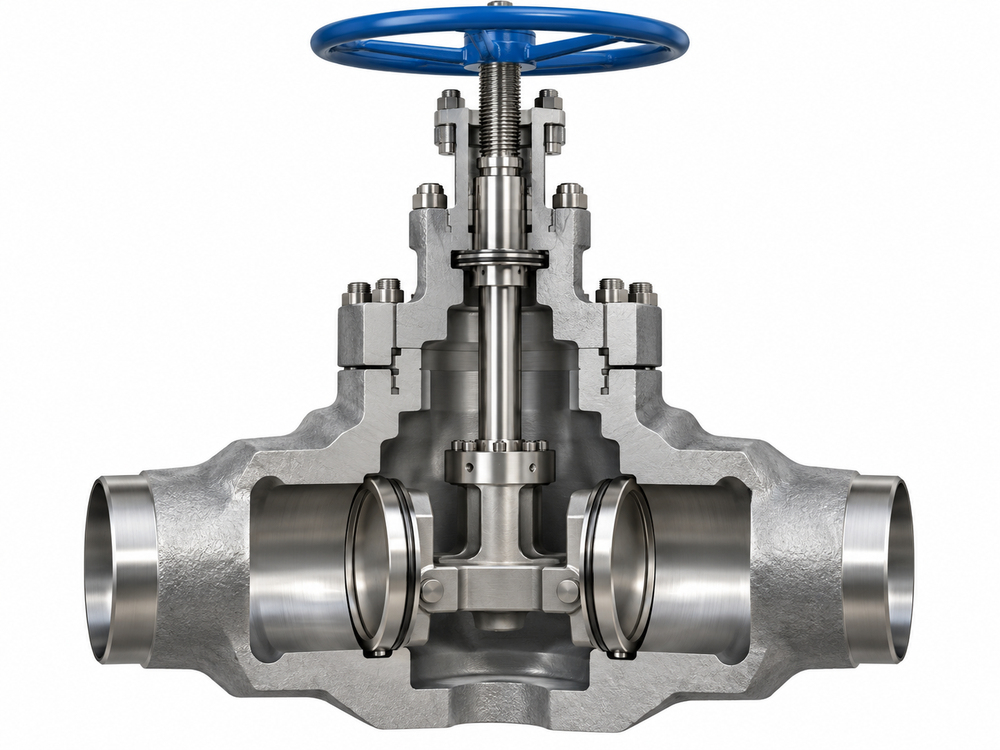
The requested gate uses two discs associated with parallel seats. The final sectional drawing should show disc guidance, the disc carrier, the mechanism maintaining seating contact, seat-ring attachment and the travel needed to clear the flow passage. The phrase “double disc” alone does not establish these details or prove that two suppliers offer interchangeable designs.
Review opening and closing loads against maximum differential pressure and thermal conditions. Any cavity-pressure provision, required flow direction or operating restriction should appear in the approved documentation. Continuous throttling should be addressed with a valve designed and qualified for that duty rather than assumed from the isolation specification.
C12A Body, F91 Trim and Stellite Documentation
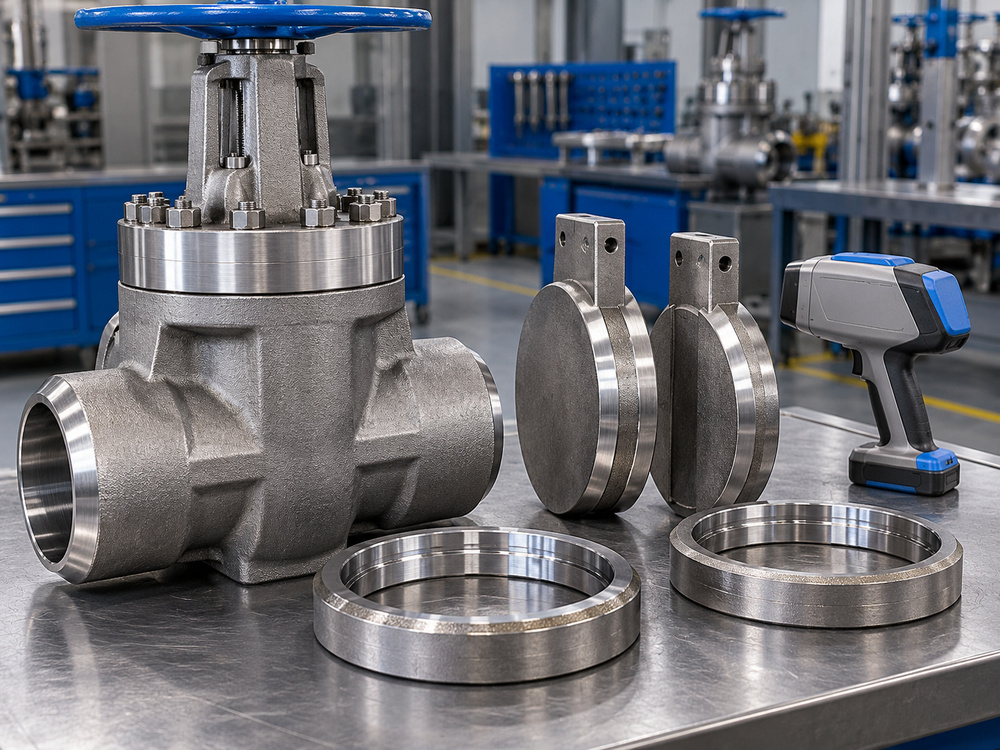
The body and internal parts have different material specifications. Matching the broad alloy family does not establish exact compliance. The manufacturer should provide a component-by-component bill of materials and identify any proposed deviation before order placement.
| Component | Required Evidence | Purchasing Check |
|---|---|---|
| C12A cast body | Material certificate, heat identification and applicable heat-treatment records | Confirm specification, grade and traceability to the actual casting |
| F91 discs and seats | Material records and approved component drawings | Confirm substrates and seat attachment; an overlay certificate alone is insufficient |
| Stellite surfaces | Specified alloy designation, application procedure and agreed hardness / examination records | Define grade, finished overlay requirements and acceptance criteria |
| Type 410 stem | Material certificate and relevant manufacturing / heat-treatment requirements | Review strength, temperature suitability and operator loads for the actual design |
PMI supports alloy identification but does not replace mechanical-property certification, heat-treatment verification or examination of the hardfaced surfaces. Request the inspection method and coverage explicitly, including whether the substrate and overlay are examined separately.
Pressure Seal Bonnet and Applicable Standards
A PSB concerns the body-bonnet pressure boundary. It does not define the gate geometry, stem packing system or seat leakage acceptance. Request the bonnet section, gasket specification, retention arrangement and assembly requirements for the offered model.
ASME B16.34 provides a valve construction and pressure-temperature framework, while ASME B16.25 addresses butt-welding end preparation. API 600 is titled for steel gate valves with bolted bonnets. For this requested PSB parallel slide configuration, the supplier must state the agreed design basis and how requested API 600 provisions are addressed. An “equivalent” designation should be supported by a technical comparison accepted by the buyer.
Keep bonnet and stem sealing terminology separate. The Bellows Seal Gate Valve uses a different stem-sealing concept; a pressure seal bonnet alone does not establish a bellows barrier.
Butt-Weld Ends, End-to-End Length and Installation Space
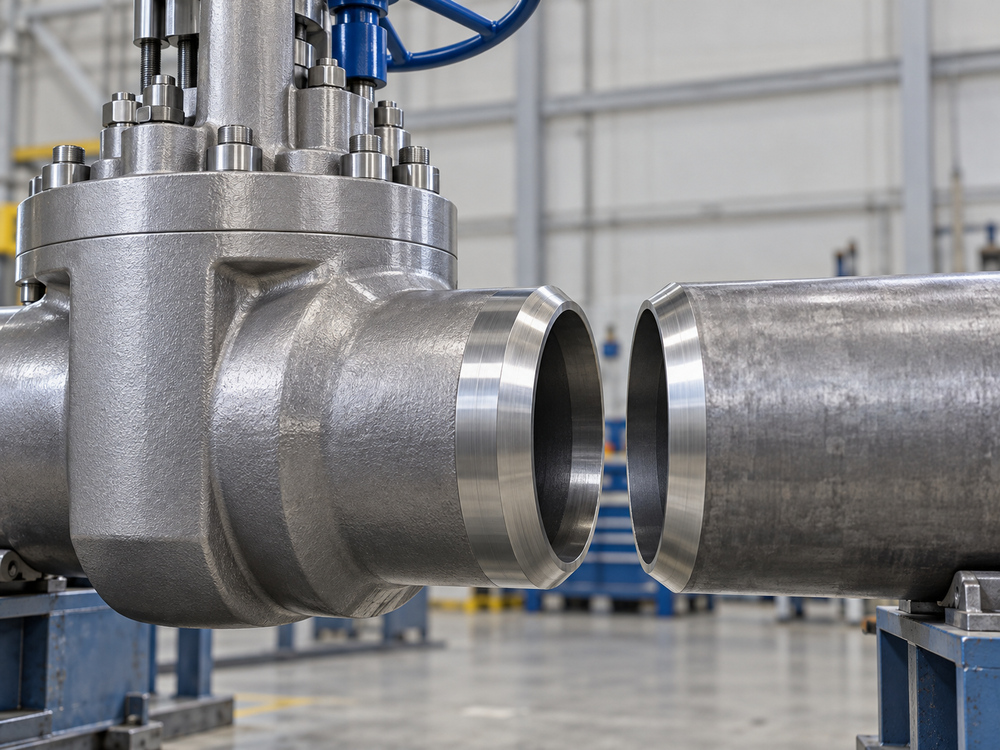
The inquiry asks for weld ends to ASME B16.25, dimensions and valve weight. To prepare a useful drawing, provide the mating pipe outside diameter, actual wall thickness or schedule, pipe material and any existing replacement-valve dimensions. Heavy-wall end shaping and internal transitions must be reviewed against the selected piping interface.
For BW construction, identify the end-to-end dimension between welding ends rather than relying on a generic flanged face-to-face value. The drawing should also state bore, overall height, operator envelope, stem travel and maintenance clearance. Supply valve weight and shipping gross weight separately for installation and transport planning.
Inspection and Certification Package
The RFQ combines mandatory document requests with items described as “if applicable” or “if available.” Resolve these conditions in the quotation so the buyer can compare offers with the same acceptance scope. Agree procedures, inspection coverage and witness points before manufacture.
| Requested Deliverable | Scope to Agree |
|---|---|
| Inspection and testing procedures | ITP, applicable test standards, acceptance criteria and buyer / third-party hold or witness points |
| Material Test Certificate | Component coverage, certificate format and linkage to heat numbers and valve identification |
| Hydrostatic test certificate | Shell test pressure, duration, test medium and acceptance under the approved standard |
| Seat leakage test certificate | Test pressure, direction(s), duration, medium and permissible leakage; no automatic zero-leakage claim |
| NDE / NDT certificate, if applicable | Method, component / weld coverage, examination stage, personnel qualification and acceptance basis |
| PMI report, if available | Parts examined, instrument / method, readings and traceability |
| Hardfacing certificate / hardness report, if available | Overlay alloy, process records, measurement locations and specified acceptance limits |
| Certificate of Origin | Required origin document format and issuing body |
| Certificate of Conformity | Statement against the purchase order, approved datasheet and documented deviations |
| Similar-service references | Verifiable Class 2500 / C12A / F91 references where available, with customer permission for disclosure |
A cold factory pressure test verifies acceptance under its stated conditions. It does not independently demonstrate hot-service operation, cycling endurance or installed plant performance. Those requirements need separate agreement if the project calls for them.
Information Needed to Finalize the Offer
- Exact medium and line duty, including whether the application is steam, feedwater or another service.
- Operating and design pressures and temperatures, startup/shutdown extremes and expected operating cycles.
- Maximum opening and closing differential pressure, operator preference and actuator requirements where relevant.
- Mating pipe OD, wall thickness / schedule, material, weld-end detail and required end-to-end length.
- Whether PSB is mandatory, and which design standards and editions the project accepts.
- Required leakage criteria, NDE coverage, PMI and hardfacing records, certificate format and inspection attendance.
If an equalizing bypass is considered, define its duty and connections during engineering review. Our steam isolation valve bypass guide distinguishes line-pressure equalization, warm-up and cavity-pressure management; these functions should not be treated as interchangeable.
Frequently Asked Questions
Is this inquiry for a globe valve or a gate valve?
The specified closure is a double disc / parallel slide gate valve. A globe valve has a different closure geometry and would be a separate selection requiring project approval.
Can a forged F91 body be quoted as exact C12A compliance?
No. The RFQ specifies ASTM A217 Grade C12A casting material. A forged-body offer must identify its actual material specification and obtain approval for the deviation.
Is PSB already confirmed in this case?
No. The inquiry requests it conditionally. The offered configuration must be made explicit before the order and approved drawing are finalized.
What is the maximum operating temperature?
No temperature limit is established by the supplied inquiry. The manufacturer must check the complete valve against the project’s design temperature, applicable rating basis and component limits.
Are dimensions, weight and all certificates already available?
They are requested deliverables, not supplied results. Confirm them against the selected design and agreed inspection scope rather than publishing assumed values.
Can this page be used as a completed supply reference?
This page is an RFQ-based procurement case. A completed supply reference requires verified order, manufacturing, test and delivery evidence.
Request a Class 2500 Parallel Slide Gate Valve Review
Send Vcore Valve your datasheet, process conditions, welding-end requirements and inspection schedule. Include the specified C12A / F91 materials and whether a pressure seal bonnet is mandatory so the proposed design, deviations, documentation scope, price and delivery time can be reviewed together.